Address
Zhengzhou, Henan, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
Zhengzhou, Henan, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM

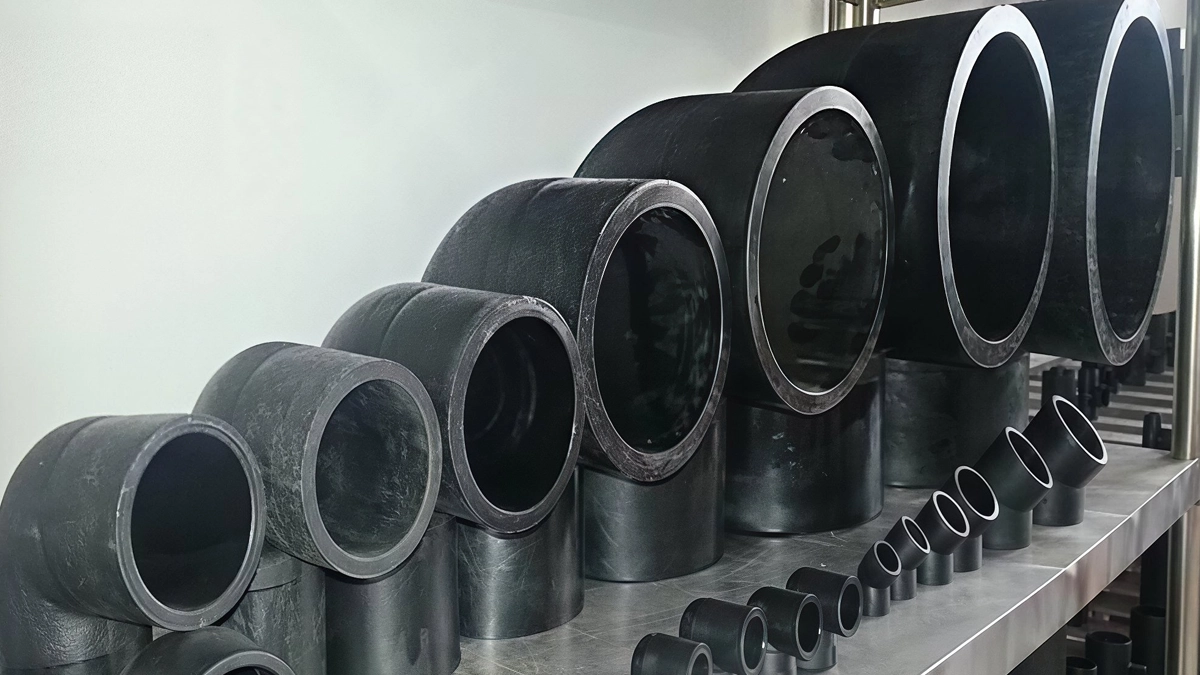
Large Diameter HDPE Elbow fittings help project teams choose the right angle, SDR, radius, and fabrication method for water, mining, and industrial pipelines, with practical guidance on performance, installation, and procurement.
High-Density Polyethylene (HDPE) elbow fittings are highly specialized, curved piping components. Their primary function? Redirecting the trajectory of fluid flow across massive industrial, municipal, and mining networks. When engineers refer to “large diameter” in this context, they mean serious scale—outside diameters stretching from 110mm all the way past 2000mm in Metric OD (ISO standards), or 4″ to 63″ in IPS (ASTM standards).
Manufacturers forge these critical components from virgin PE100 or PE4710 resins, yielding a dense material profile of roughly 0.95 to 0.96 g/cm³. That tightly packed molecular structure is exactly what allows the fitting to handle immense internal pressure without flinching. Top-tier producers like JINQUAN leverage massive infrastructure—including a 200-acre facility pushing out over 100,000 tons annually—to build these elbows to strict project specifications, keeping complex global pipelines moving seamlessly.
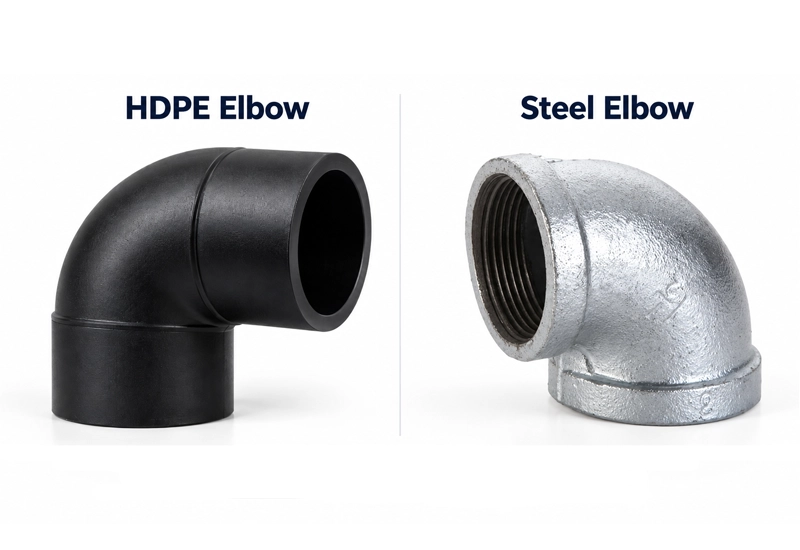
Pipeline contractors and system designers consistently choose large diameter HDPE elbows over traditional metal fittings. The decision comes down to a rare mix of physical toughness, chemical immunity, and structural continuity.
Picking the right manufacturing style for your elbow dictates how well the pipeline handles pressure ratings and fluid dynamics. Industrial applications generally rely on three distinct configurations.
Injection Molded Elbows
Created by forcing molten PE100 resin directly into a steel mold, these are entirely seamless HDPE pipe fittings. You will typically find them in sizes up to 315mm or 400mm. Molded elbows feature a tight, abrupt turning radius (usually 1D to 1.5D). Because they lack seams, they carry the full pressure rating of the adjacent pipe—no derating calculations required.
Fabricated (Segmented/Mitered) Elbows
When projects demand massive diameters (up to 2000mm) that simply cannot be molded, fabricated elbows step in. Manufacturers build these by cutting straight HDPE pipe into precise angular segments (like 11.5° or 22.5°) and butt-fusing them together to form 45° or 90° bends. Because those mitered joints introduce internal flow turbulence and create localized stress points, engineers must apply pressure derating to these HDPE fittings.
Sweep Bends
Instead of cutting and fusing, sweep bends are made by heating and mechanically curving a single, continuous length of HDPE pipe. They boast a long, gradual radius (such as 3D, 5D, or 8D). This gentle curve drastically cuts down internal friction, minimizes pressure drops, and smooths out fluid turbulence. If you are moving high-velocity abrasive slurries, sweep bends are the absolute best choice.
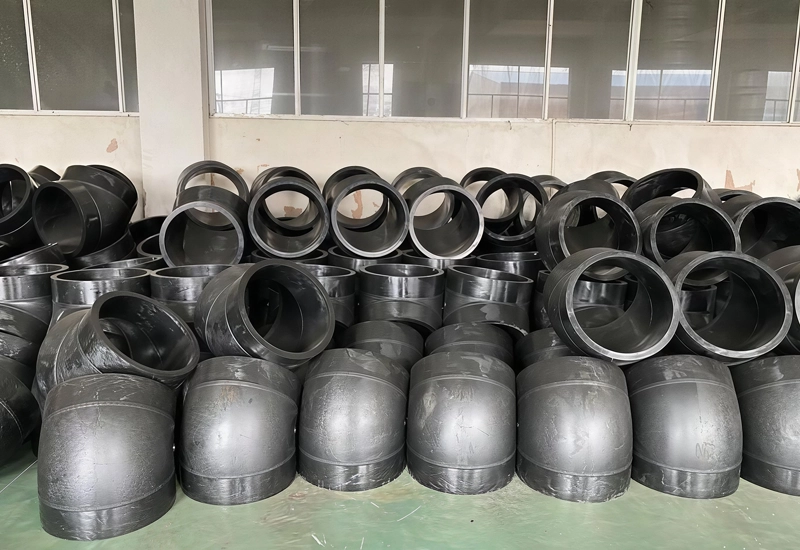
Sourcing the right large diameter fitting means locking down exact dimensional and material data. Guesswork here leads to fusion misalignment on the job site.
| Specification | Measurement / Standard |
|---|---|
| Diameter Range | DN110 to DN2000 (Metric OD) / 4" to 63" (IPS) |
| SDR (Standard Dimension Ratio) | SDR 11, SDR 13.6, SDR 17, SDR 21, SDR 26 |
| Pressure Class (PN) | PN6 (SDR26), PN8 (SDR21), PN10 (SDR17), PN12.5 (SDR13.6), PN16 (SDR11) |
| Standard Angles | 22.5°, 30°, 45°, 60°, 90° |
| Bend Radius | Short Radius (1D – 1.5D), Long Radius/Sweep (2D, 3D, 5D) |
| Material Grade | PE100, PE80, PE4710 |
| Manufacturing Standards | ISO 4427 (Water), EN 12201, ASTM F714, GB/T13663 |
Comparing elbow configurations side-by-side helps procurement teams balance immediate material costs against long-term operational performance.
| Feature | HDPE Molded Elbow | HDPE Fabricated Bend (Mitered) | Steel Elbow |
|---|---|---|---|
| Corrosion Resistance | Excellent (Immune) | Excellent (Immune) | Poor (Requires coating/lining) |
| Weight | Lightweight (~1/8th of steel) | Lightweight | Very Heavy |
| Installation Speed | Fast (Butt Fusion) | Fast (Butt Fusion) | Slow (Welding/Flanging) |
| Pressure Rating | Full Rating | Reduced (Requires Derating) | Full Rating |
| Flow Efficiency | Moderate (Short Radius) | Lower (Turbulence at seams) | Moderate to High |
| Lifecycle Cost | Low (50-100 year life) | Low | High (Maintenance/Replacement) |
Large diameter HDPE elbows form the backbone of sectors where fluid security and long-term durability are critical.
Mining and Slurry Operations
Consider a gold mining operation in Colombia that struggled with constant abrasion blowouts. The facility used a standard 160mm PN16 steel-lined pipe at a gravimetric concentrator discharge, but the abrasive slurry chewed through the metal, forcing full replacements every month or two. The solution? Swapping to specialized PE100 sweep elbows fitted with mechanical flanges. Installation took just 20 minutes. More importantly, the new HDPE system maintained flawless structural integrity and perfect hermeticity well past 90 days of relentless, abrasive flow.
Municipal Water Transmission
City planners favor large diameter elbows for their seismic resilience. Because butt-fused joints are monolithic and flexible, they absorb ground shifts and earthquake tremors without cracking. This flexibility also makes them the go-to choice for trenchless installations like horizontal directional drilling (HDD).
Industrial Processing
Chemical plants and processing facilities rely on these heavy-duty elbows to move aggressive fluids safely. Whether handling highly acidic tailings, heavy dredging lines, or toxic chemical leachate, HDPE ensures the zero-leakage performance these dangerous applications demand.
Matching the fitting to the environment requires precise engineering alignment. Run through these criteria to verify your project parameters before purchasing.
1. Verify the Sizing Standard: Identify whether your pipeline network runs on Metric OD (ISO 4427) or IPS/DIPS (ASTM F714). Mixing these standards guarantees fusion failure.
2. Calculate Pressure Derating (EDR): Fabricated mitered elbows inherently lose some pressure capacity due to their segmented seams. A standard industry practice is to specify a fitting with a Dimension Ratio (DR) one step lower (which means a thicker wall) than the main pipe. For instance, pairing a DR 9 fabricated fitting with a DR 11 pipeline ensures consistent pressure handling across the entire system.
3. Select the Manufacturing Type: Use molded elbows for high-pressure networks in confined spaces. Shift to fabricated elbows for massive diameters over 400mm. Specify sweep bends if you are pumping abrasive, high-velocity slurries.
4. Confirm Angle and Radius: Define the exact directional change needed (e.g., 45° or 90°). Then decide if your system’s flow dynamics require a short 1.5D radius or a long, sweeping 3D/5D radius.
5. Check Required Certifications: Ensure your components meet regional and application-specific standards. Look for ISO 4427, CE, WRAS (if handling potable water), or specific SGS testing validations.
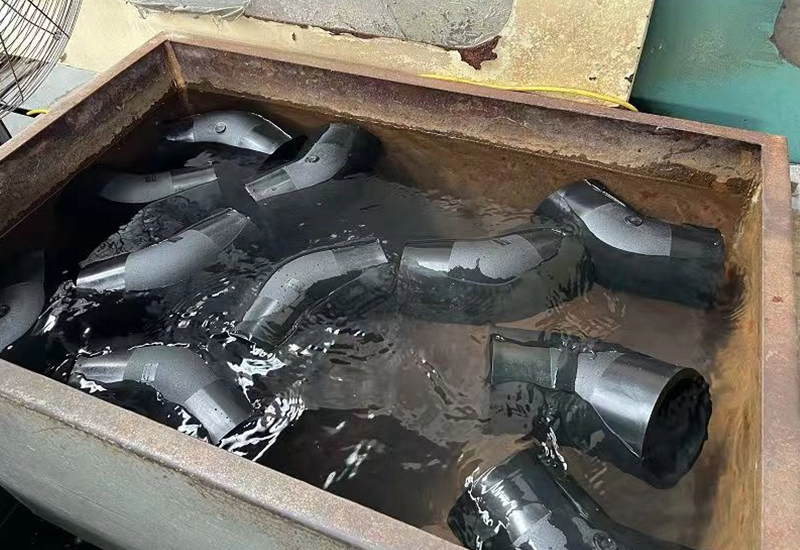
A large diameter HDPE elbow is only as reliable as the butt fusion joint connecting it to the grid. Executing this process flawlessly guarantees a leak-free connection built to last decades.
1. Inspection and Cleaning: Start by rigorously inspecting the pipe ends and the elbow. Wipe away all dirt, moisture, oil, and debris from both the polymer surfaces and the fusion machinery.
2. Alignment and Clamping: Lock the straight pipe and the elbow into the hydraulic fusion machine. Adjust the clamps until the alignment is dead-on—there should be zero high/low offset between the inner walls.
3. Facing: Engage the mechanical facer to shave both pipe ends at the same time. This step exposes fresh, clean polymer and guarantees the two surfaces are perfectly parallel.
4. Heating: Insert the PTFE-coated heater plate (strictly calibrated between 400-450°F / 204-232°C). Apply moderate pressure until a uniform melt bead forms around the entire circumference.
5. Fusion: Quickly extract the heater plate. Press the molten ends together using the exact hydraulic force specified for the pipe size, and hold it steady.
6. Cooling and Testing: Maintain that pressure until the joint cools completely to the ambient air temperature. Never skip the final hydrostatic pressure test on the pipeline segment before fully commissioning the system.
For procurement teams, buying large-scale pipeline components means balancing complex cost drivers against supplier reliability.
Cost Drivers Breakdown:
Supplier Evaluation:
Working directly with a factory manufacturer cuts out middlemen and prevents project delays. JINQUAN provides major procurement advantages, including aggressive lead times of just 7 to 15 days, flexible Minimum Order Quantities (MOQs), and ready-to-ship samples for quality checks. Backed by an annual output capacity exceeding 100,000 tons and rigorous export packaging standards, JINQUAN ensures massive infrastructure builds hit their deadlines without blowing the budget.
A successful pipeline installation hinges on getting the details right: matching the exact outside diameter and SDR, accurately factoring in pressure derating for fabricated fittings, and executing perfect on-site butt fusion. By teaming up with a high-capacity, fully certified manufacturer, engineering and procurement teams secure strict technical compliance and ensure the long-term commercial success of their infrastructure investments.
What diameter range is considered a large diameter HDPE elbow?
In the municipal and industrial sectors, “large diameter” typically covers sizes from 110mm up to 2000mm and beyond when measuring by Metric Outside Diameter (OD). If you are operating in the North American market using IPS (Iron Pipe Size) standards, this translates to 4 inches up to 63 inches.
Can HDPE elbows be used in mining slurry pipelines?
Absolutely. In fact, they are the preferred choice. High-density polyethylene boasts incredible abrasion resistance, easily outlasting steel by up to four times in sliding-bed slurry networks. Engineers frequently spec long-radius sweep elbows for these jobs to minimize internal turbulence and drastically reduce wear from abrasive particles.
Which is better for large diameter HDPE pipelines: molded elbows or fabricated elbows?
For sizes up to 400mm, molded elbows take the lead because they maintain 100% of the pipe’s pressure rating without any need for derating. However, once a pipeline exceeds 400mm, fabricated (mitered) elbows become the necessary standard. Just remember that fabricated fittings require precise pressure derating calculations to offset the structural stresses at their fused seams.
How do I choose the correct SDR for pressure service?
The Standard Dimension Ratio (SDR) simply compares the pipe’s diameter to its wall thickness. A lower SDR equals a thicker wall and higher pressure tolerance (for example, SDR 11 handles PN16, while a thinner SDR 17 handles PN10). When installing fabricated elbows, a good rule of thumb is to select a fitting with an SDR one step lower than your main pipeline to safely offset pressure derating.
How are large diameter HDPE elbows joined to pipe sections?
Contractors primarily use butt fusion welding. This thermal process melts the pipe ends and presses them together, forming a seamless, monolithic bond. If the pipeline needs to transition to steel pipes, heavy valves, or pumps, crews use mechanical flange adapters (which consist of an HDPE stub end paired with a steel backing ring).
What information should I provide to get an accurate custom quote?
To speed up the quoting process and ensure accuracy, provide the exact Outside Diameter (specifying Metric or IPS), the required pressure rating (PN) or SDR, the angle of the bend (like 45° or 90°), the bend radius (short or long sweep), the raw material grade (PE80 or PE100), and the exact manufacturing standard required (such as ASTM F714 or ISO 4427).
Do HDPE elbows need special support or anchoring in long pipeline runs?
Unlike old-school bell-and-spigot PVC or ductile iron setups, fully butt-fused HDPE systems are self-restraining. This means you do not need concrete thrust blocks at directional changes. However, because polyethylene expands and contracts with temperature changes, long above-ground runs might still require engineered guide supports or specific trench embedment techniques.
Large diameter HDPE elbow fittings serve as the structural anchor for the safe, leak-free transport of municipal water, harsh industrial chemicals, and abrasive mining slurries. By mastering the physical differences between injection molded, fabricated mitered, and long-radius sweep bends, system designers can easily optimize both pressure integrity and fluid dynamics. Following strict SDR guidelines, properly calculating pressure derating, and executing flawless butt fusion welds are non-negotiable steps for mitigating risk. When procured from a proven, high-volume manufacturer and installed with precision, these rugged components deliver a resilient, maintenance-free pipeline designed to operate flawlessly for 50 to 100 years.