Address
Zhengzhou, Henan, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
Zhengzhou, Henan, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM

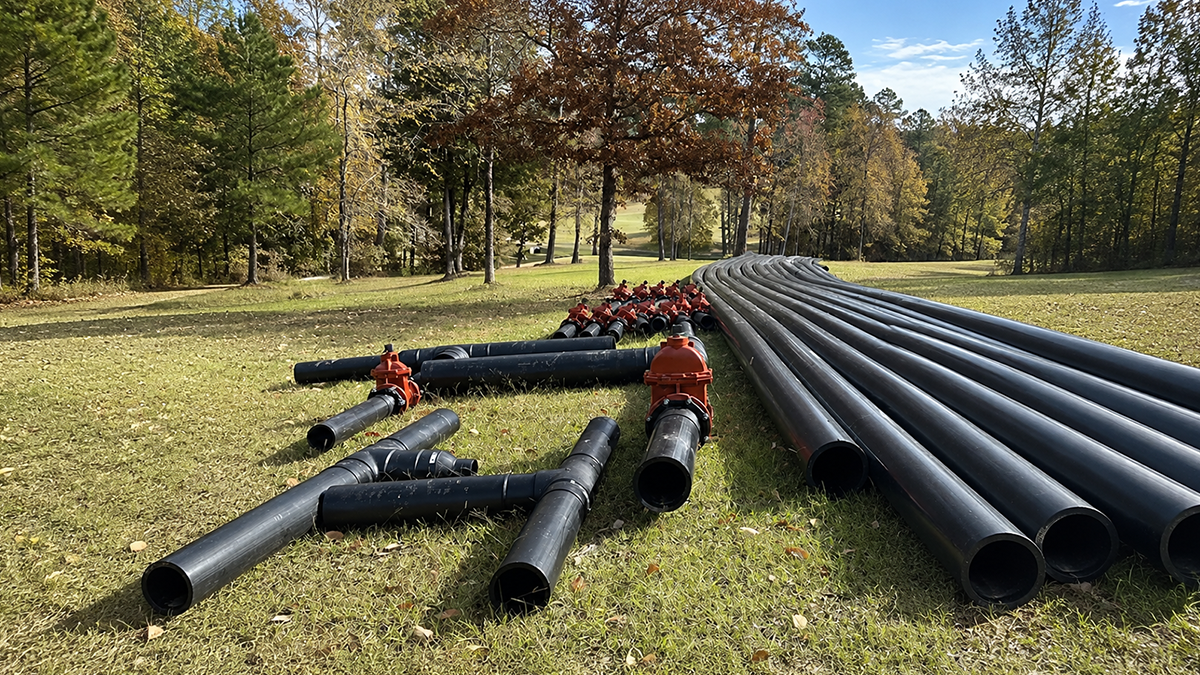
HDPE Elbow Fittings help engineers and buyers match size, angle, SDR, and pressure class to pipeline needs. This guide explains types, standards, uses, and selection factors for reliable, cost-effective installations.
Changing the direction of fluid flow in a thermoplastic pipeline demands reliable components. That’s where HDPE (High-Density Polyethylene) elbow fittings come in. Extruded from PE80 or PE100 petroleum-based polymers, these fittings drop the need for clunky mechanical joints. Instead, they rely on heat fusion to forge a seamless, leak-proof network.
What makes HDPE stand out? It’s the material’s unique physical traits. With a density sitting between 0.941 and 0.965 g/cm³ and a tensile strength hitting 20–30 MPa, you get an incredible strength-to-density ratio. Better yet, HDPE is highly ductile. This means the elbows can absorb intense operational stresses and water hammer shocks up to 2,500 times better than rigid PVC alternatives. Blending flexibility with raw strength, these fittings form the backbone of modern, high-performance piping infrastructure.
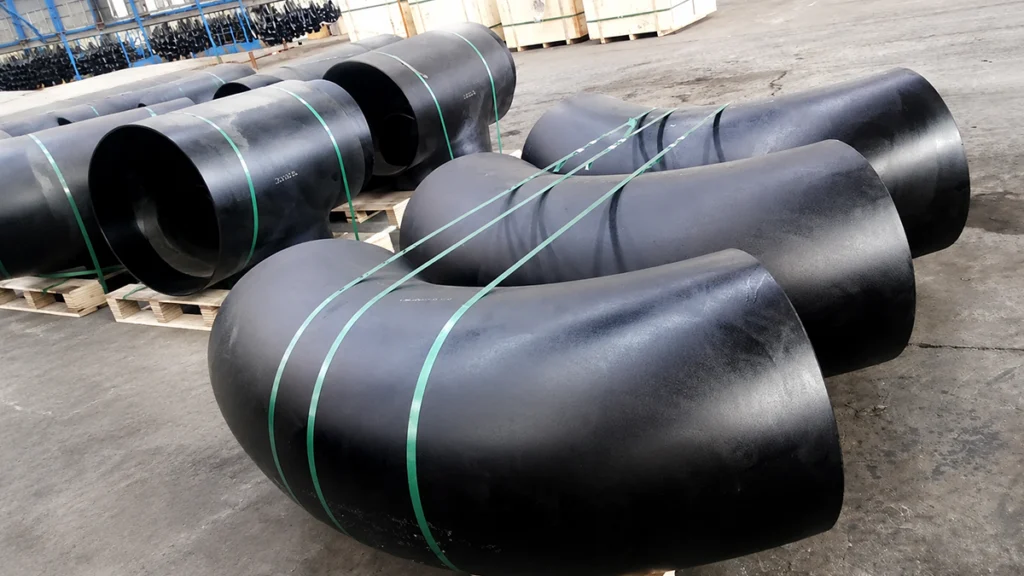
Routing a HDPE pipe rarely means traveling in a perfectly straight line. To handle precise directional shifts, manufacturers produce HDPE elbows using two primary methods—injection molding and custom fabrication—to match virtually any trajectory.
Standard Molded Angles
Injection-molded elbows dominate standard HDPE pipeline turns. You’ll find them universally available in 90°, 45°, 22.5°, and 11.25° configurations. Because they are formed as a single solid piece under extreme pressure, these elbows deliver highly uniform wall thickness alongside maximum structural integrity.
Fabricated Angles
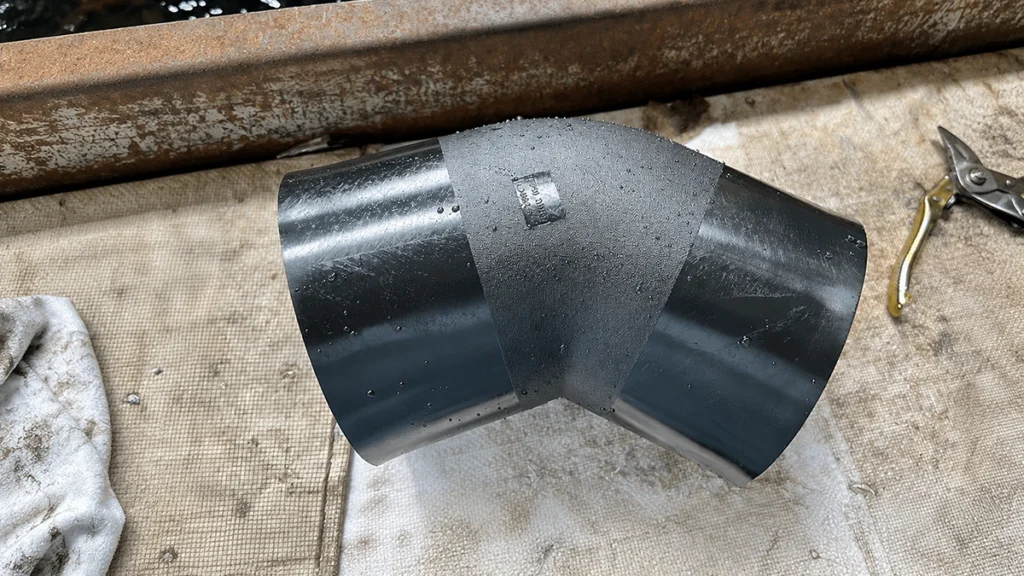
When a project demands non-standard routing or involves massive HDPE pipe diameters, custom mitered (or fabricated) elbows step in. Facilities can build these in 60°, 30°, or completely custom angles using segmented configurations made of two, three, or five pieces.
If you specify fabricated elbows, you absolutely must apply the industry-standard fabrication derating rule. Mitered joints inherently experience a drop in their pressure rating. To compensate, engineers must select a fitting with a Dimension Ratio (DR) one step lower than the main HDPE pipe, which provides a thicker wall. For instance, if your main PE pipeline runs on DR 11 pipe, you need to specify a DR 9 fabricated elbow to preserve the system’s overall pressure integrity.
Getting the size right means perfectly aligning the physical dimensions of the HDPE elbow with the pressure demands of your system. You have plenty of options, as these elbows cover a massive size range—from a compact DN16 all the way up to DN3000 (Metric), or 1/2″ to 48″ in IPS/DIPS standards.
The most vital metric to verify is the Standard Dimension Ratio (SDR). This number represents the ratio of the outside diameter to the HDPE pipe’s wall thickness. A lower SDR translates to a thicker wall, which directly yields a higher pressure rating. Keep in mind that Nominal Pressure (PN) ratings use a baseline fluid temperature of 20°C (68°F).
| SDR Rating | PN (Bar) | Pressure (PSI) | Typical Application |
|---|---|---|---|
| SDR 7.4 | PN 25 | 362.5 PSI | High-pressure mining operations |
| SDR 9 | PN 20 | 290.0 PSI | Industrial process lines |
| SDR 11 | PN 16 | 232.0 PSI | Potable water distribution |
| SDR 13.6 | PN 12.5 | 181.3 PSI | Sewer force mains |
| SDR 17 | PN 10 | 145.0 PSI | Transmission mains |
| SDR 21 | PN 8 | 116.0 PSI | Low-pressure distribution |
| SDR 26 | PN 6.3 | 91.0 PSI | Gravity sewage systems |
Temperature Derating: Remember that the nominal pressure (PN) holds true only up to 20°C. Once fluid temperatures climb to 40°C (104°F), you have to apply a derating factor of 0.74 to the maximum allowable system pressure. Skipping this step risks catastrophic material failure.
Manufacturers build and test HDPE elbow fittings against rigorous international standards to guarantee global compatibility and onsite safety. The most critical specifications include ISO 4427 and EN 12201 for plastic water supply systems, ASTM D3261 covering butt heat fusion PE fittings, AWWA C906 for polyethylene pressure HDPE pipes, and ASTM F2206 for fabricated fittings.
Once onsite, integrating these components into the wider pipeline requires specialized thermal joining techniques:
Thanks to their incredible versatility and high chemical resistance, HDPE elbows serve a wide variety of infrastructure and industrial sectors.
Nailing the exact specifications for your elbow prevents disastrous system failures while securing long-term efficiency. Run through these core selection criteria when mapping out project requirements:
1. Match the SDR/PN Rating: Confirm that the fitting’s pressure class meets—or ideally exceeds—the HDPE pipeline’s maximum sustained operating pressure.
2. Apply Temperature Derating Factors: Does your system run hotter than 20°C? If so, multiply the baseline rating by the correct factor (like 0.74 for 40°C environments) to find your true allowable pressure.
3. Account for Surge Pressures: Always factor in transient spikes. As an example, an SDR 17 PE100 elbow rated for 10 Bar of static pressure can easily handle transient water hammer shocks up to 15 Bar.
4. Choose Molded vs. Fabricated: Stick to injection-molded elbows for standard, high-pressure tasks. Save fabricated elbows for massive diameters or unique custom angles, and always enforce the DR step-down rule.
*Case Example:* Imagine a municipal gravity sewer running at ambient temperatures. An injection-molded SDR 26 90-degree HDPE elbow handles this flawlessly. But if that exact same municipality builds a pressurized sewer force main prone to water hammer, they have to upgrade the spec. Switching to an SDR 13.6 or SDR 11 elbow becomes mandatory to absorb those elevated transient stresses.
When weighing PE pipeline materials against each other, HDPE elbows bring distinct benefits to the table—especially regarding long-term durability and the installation process—that traditional rigid plastics and metals struggle to match.
| Feature | HDPE Elbow Fittings | PVC Elbow Fittings | Steel Elbow Fittings |
|---|---|---|---|
| Material Structure | Semi-crystalline and ductile | Amorphous and rigid | Metallic alloy |
| Impact Resistance | High; withstands sub-zero impacts | Low; susceptible to brittle cracking | Very High |
| Tensile Strength | 20–30 MPa | ~50 MPa | 400+ MPa |
| Joining Method | Leak-free heat fusion | Solvent cement or mechanical gaskets | Welding or mechanical flanging |
| Corrosion & Scale | 100% resistant; immune to scale | Resistant | Susceptible; requires cathodic protection |
| Best Use Case | Water/wastewater under 25 Bar | Low-cost residential plumbing | Extreme high-pressure lines |
Steel certainly dominates extreme high-pressure environments pushing past the 25 Bar mark. However, HDPE weighs a fraction of metallic alternatives, completely resists internal scale buildup, and bypasses the need for costly cathodic protection systems. When matched against PVC, the ductile nature of HDPE shines. It easily absorbs heavy impacts and survives sub-zero temperatures without suffering from the brittle cracking that plagues rigid plastics.
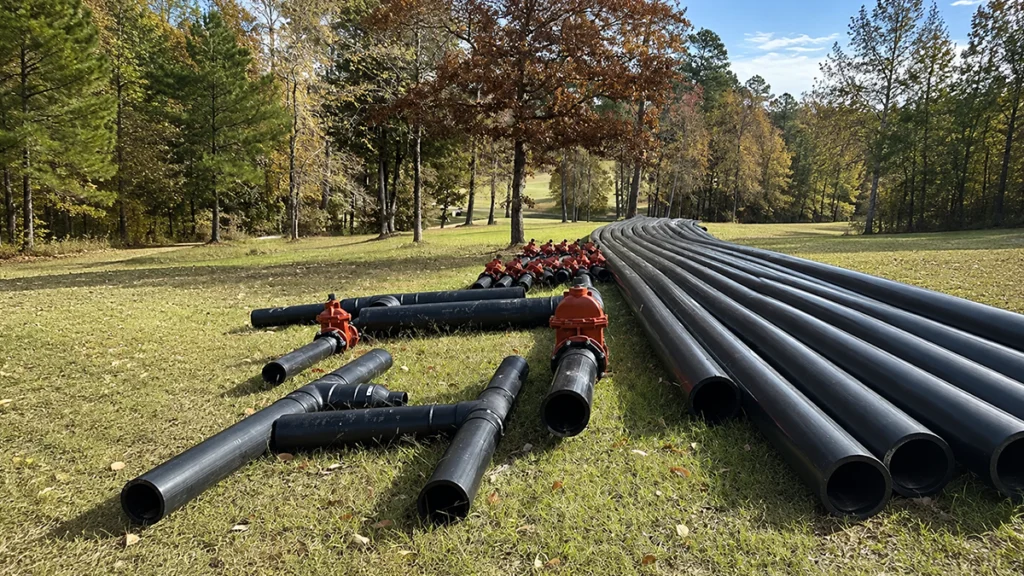
Getting installation and testing right is non-negotiable. If you want a monolithic, leak-free pipeline, your butt fusion workflow needs to follow incredibly strict parameters:
1. Preparation: Thoroughly clean and face both the pipe and fitting ends. You need perfectly parallel, uncontaminated surfaces before applying any heat.
2. Heating: Press the heater plate against the prepared surfaces. For butt fusion, hold the temperature tightly between 400°F and 450°F.
3. Joining: Pull the heater plate away and press the molten surfaces together, strictly applying the manufacturer’s specified interfacial pressure.
4. Cooling Phase: Never rush this step—it is the most critical part of the process. Calculate your cooling time in minutes by multiplying the wall thickness (in mm) by `1.15 to 1.33`. The joint absolutely must cool below 70°C (158°F) before you release the clamping pressure, giving the polymer time to fully recrystallize.
Testing Procedures: Once installed, hydrostatic pressure testing must adhere to ASTM F2164 guidelines. You must use water as the test medium. Compressed air is incredibly dangerous; its compressibility creates a massive explosion risk if a joint fails. Finally, operators need to wait a minimum of four times the total fusion cooling time before starting any pressure tests.
Sourcing industrial pe pipeline components isn’t just about finding the right price. You have to vet the manufacturing facility to confirm their capacity, compliance standards, and overall reliability.
Factory Capabilities: Always verify the operational scale of the manufacturer. Take JINQUAN as an example: operating out of a 200-acre facility with more than 60 injection molding machines, they push an annual production capacity past 100,000 tons. Scale like this guarantees that massive bulk orders get fulfilled without frustrating delays.
Quality and Certification: Don’t take quality for granted. Check that the supplier actively holds ISO 9001 for quality management and ISO 14001 for environmental management, along with CE and SGS certifications. These credentials prove the elbows actually meet stringent ISO 4427 and ASTM standards.
Logistics and Lead Times: Working directly with factory manufacturers unlocks serious supply chain perks. Look for rapid lead times—usually hovering between 7 and 15 days. You also want a partner offering OEM/ODM customization for those specialized fabricated fittings, readily available sample products for quality checks, and heavy-duty export packaging that keeps components safe during rough international transit.
Getting the specification right sets the foundation for total pipeline integrity. When you draft procurement documents, avoid vague, generic descriptions. Start by specifying the exact material grade—whether PE80 or PE100—to lock in the baseline strength. Clearly outline the required angle and dictate whether the fitting must be injection-molded or custom-fabricated. Next, define the exact SDR or PN rating driven by your maximum operating pressure, making sure to calculate temperature and surge derating. Lastly, call out the specific joining method (like butt fusion versus electrofusion). This ensures the physical dimensions and component designs perfectly match the contractor’s field equipment.
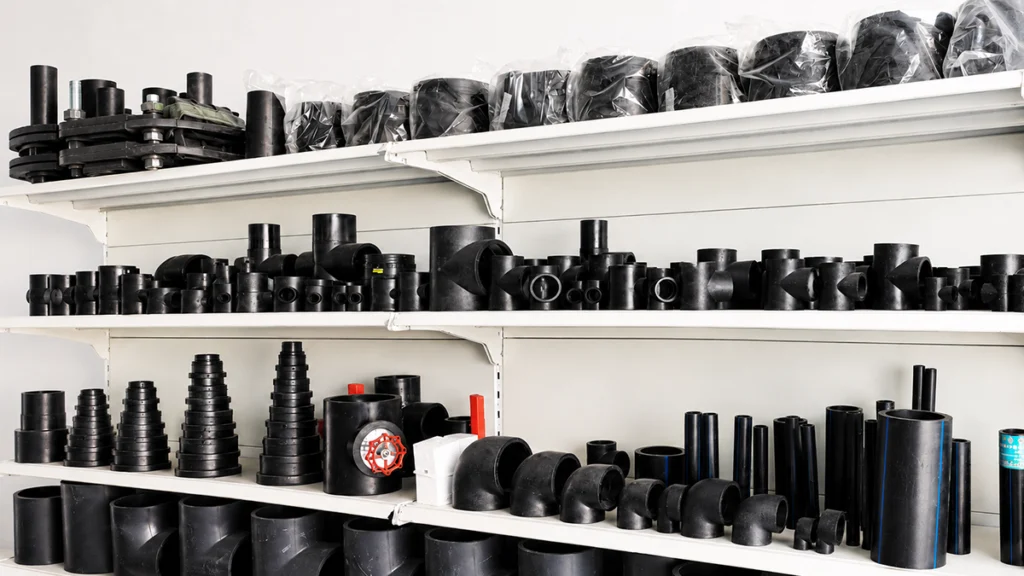
You can source HDPE elbow fittings across a massive size spectrum, covering everything from minor distribution lines to heavy civil infrastructure. In metric dimensions, they range from DN16 up to a massive DN3000. If you use IPS (Iron Pipe Size) or DIPS (Ductile Iron Pipe Size) standards, that translates to sizes from 1/2″ all the way up to 48″.
A 90-degree elbow forces a sharp, right-angle turn. While great for tight, restricted routing, it does create higher friction loss. Conversely, a 45-degree elbow offers a much gentler directional shift. This reduces fluid turbulence and minimizes pressure drops, making it the better choice for maximizing flow efficiency.
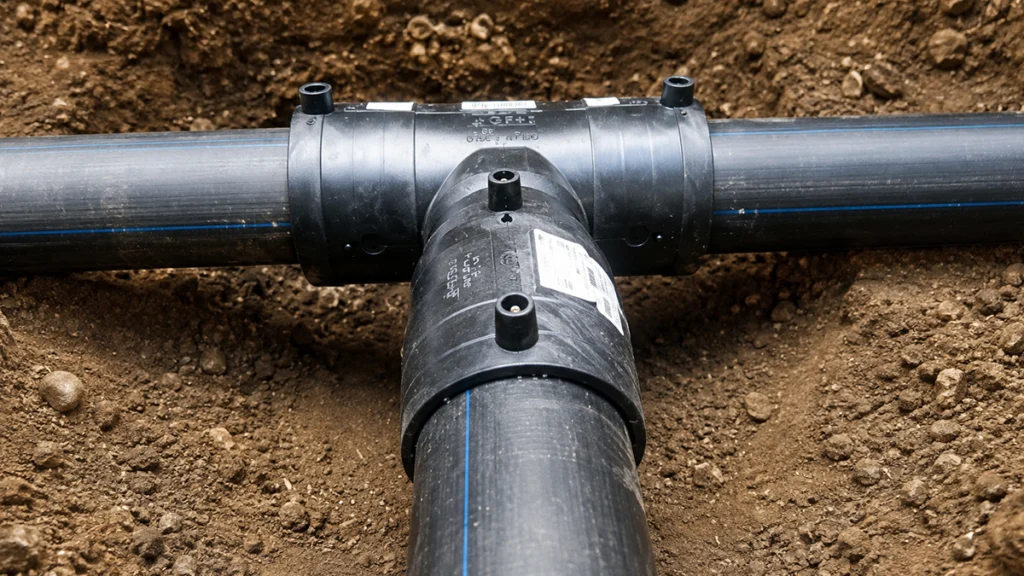
Yes, both methods work perfectly. Butt fusion involves heating the bare pipe and fitting ends to between 400°F and 450°F before pressing them together. Electrofusion takes a different route, using a specialized fitting packed with internal wire coils that automatically heat and melt the joint. It’s an absolute lifesaver for repairs in tight trenches where bulky machines can’t fit.
Start by matching the fitting’s nominal pressure (PN) to your system’s highest sustained operating pressure. The SDR (Standard Dimension Ratio) dictates the wall thickness—the lower the SDR number, the thicker the wall and the higher the pressure capacity. Don’t forget to apply a temperature derating factor if your fluid runs hotter than 20°C (68°F).
Without a doubt. For potable drinking water, they carry strict NSF/ANSI 61 certifications to guarantee public safety. On the wastewater side, their total immunity to corrosion and destructive hydrogen sulfide gas makes them vastly superior to legacy steel or concrete pipes for gravity sewers and force mains.
If you specify, install, and fuse them correctly, HDPE elbow fittings boast an impressive design life of 50 to 100 years. Because of their semi-crystalline polymer structure, they shrug off scaling, rust, biological growth, and chemical attacks. This results in decades of reliable performance with practically zero maintenance.
To get a precise quote without the back-and-forth, send the exact diameter (DN or IPS), the specific angle (like 90° or 45°), the SDR or PN pressure rating, and the material grade (PE100). Also, include your intended joining method, the project application (e.g., gas, mining, water), and the total volume you need.
Picking the right HDPE elbow fittings comes down to a deep understanding of your system’s unique demands, the operating environment, and the material’s physical limits. When engineers accurately pair the Standard Dimension Ratio (SDR) and pressure ratings with real-world operational parameters—and strictly follow rules for temperature derating and fabrication step-downs—they guarantee decades of flawless, leak-free performance. It doesn’t matter if you are ordering standard injection-molded components for a high-pressure municipal water grid or custom-fabricated elbows to navigate a complex mining slurry route. Putting certified materials and flawless thermal fusion techniques first remains the ultimate key to safeguarding your entire pipeline infrastructure.