Address
Zhengzhou, Henan, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
Zhengzhou, Henan, China
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM

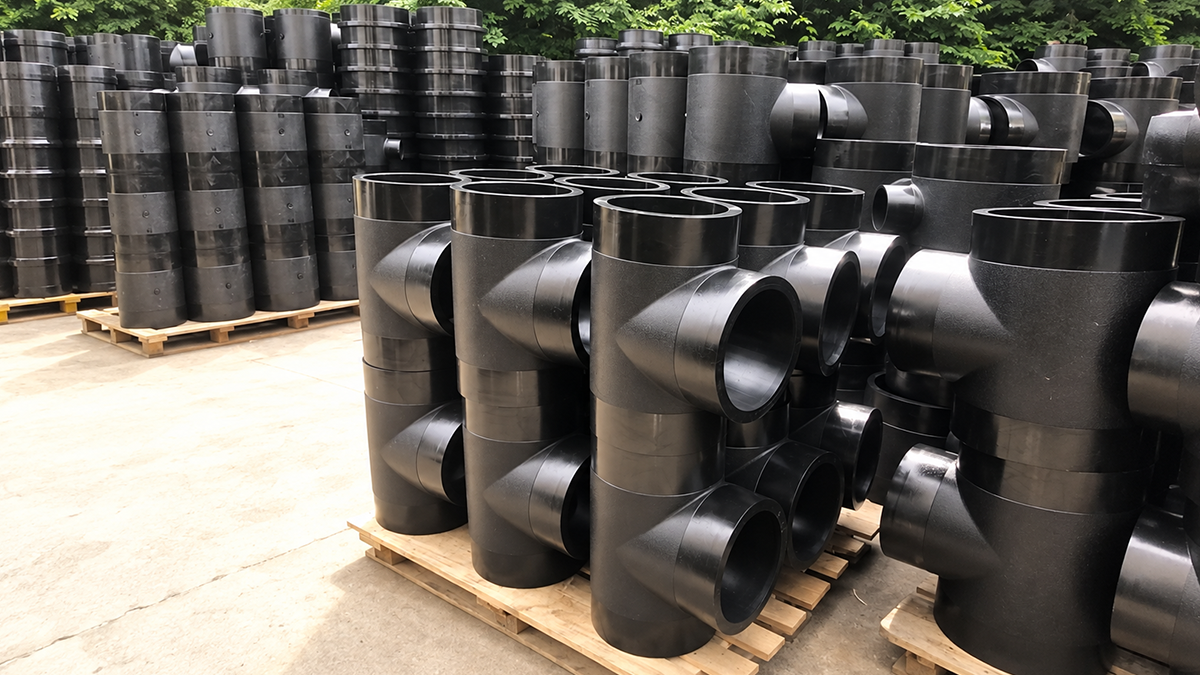
This guide compares the top 10 HDPE butt fusion fittings manufacturers by certifications, size range, application fit, price, MOQ, and lead time, helping B2B buyers, distributors, and project engineers select the right supplier with confidence in 2026.
Thermoplastic piping components like elbows, tees, reducers, and stub ends make up the core of butt fusion HDPE pipe fittings. They exist specifically to join High-Density Polyethylene pipes. How does it work? You heat both the pipe and fitting ends until they melt—usually hitting that sweet spot between 200°C and 220°C—and then press them together using controlled hydraulic pressure. This technique forms a solid, leak-proof joint. Hitting a Q-factor above 0.9 under ISO 13950 standards means this connection actually matches or beats the strength of the pipe itself.
Picking the right manufacturer isn’t just a procurement checkbox; it dictates your pipeline’s survival. Shoddy manufacturing triggers dimensional headaches, like Standard Dimension Ratio (SDR) mismatches that completely ruin a weld. Worse, lower-tier suppliers frequently sneak in non-virgin regrind plastics. That is a fast track to catastrophic pipeline blowouts. Just one compromised fitting can drag down the pressure rating of an entire network, turning a robust PN16 water system into a vulnerable PN10 liability overnight.
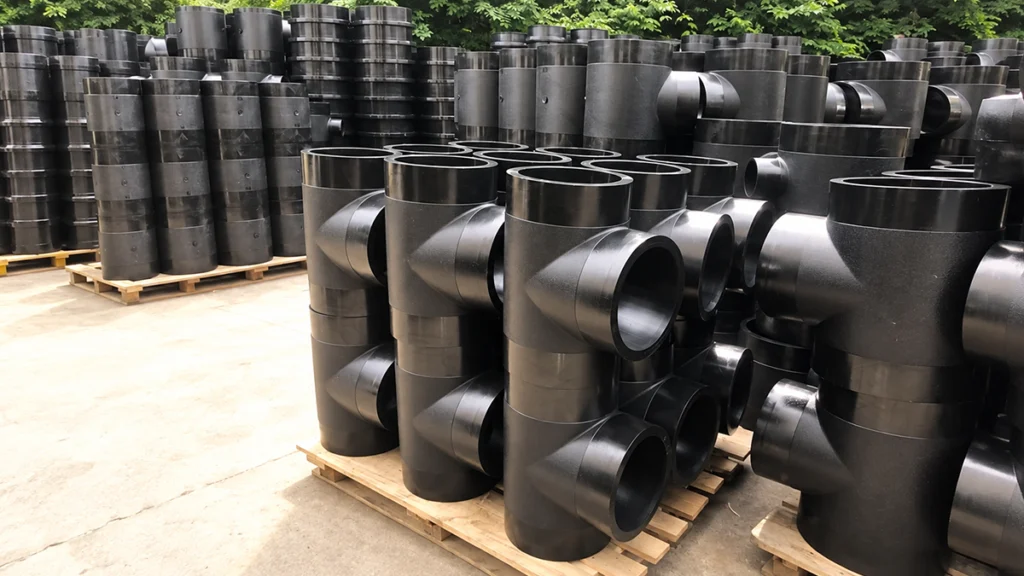
The global landscape for HDPE pipes and fittings is surging. Analysts expect the market to hit $14.10 billion by 2026, riding a 6.2% compound annual growth rate (CAGR), before climbing to a staggering $37.93 billion by 2034. Look at 2024 alone: buyers snapped up roughly 836 million fusion fittings worldwide. Those components anchored more than 4.5 million kilometers of new HDPE pipelines.
Distinct regional hubs offer unique perks for B2B buyers:
Finding a truly reliable supplier for water and gas networks requires cutting through the marketing fluff. We stripped away the sales pitches and ranked global manufacturers using a rigorous, data-centric framework anchored in international standards and actual factory floor capabilities.
1. Core International Standards: A top-tier factory must prove compliance with ISO 4427-3 (Plastics piping systems for water supply) or EN 12201-3 (PE pipes and fittings for water supplies).
2. Potable Water Certifications: ISO 4427 handles dimensions and strength, but it ignores drinking-water safety. Elite manufacturers step up with WRAS (UK) or NSF/ANSI/CAN 61 (USA/Canada) credentials.
3. Material Grade Verification: Real quality demands 100% virgin PE100 or PE4710 compounds. We checked for strict material traceability and adherence to PE100+ Association mandates.
4. Manufacturing Standards: You cannot compromise on fusion equipment compatibility (ISO 12176-1) or butt fusion jointing procedures (ISO 21307).
5. Factory Capabilities: The absolute best facilities run extensive injection molding lines capable of handling massive diameters (up to DN1200+). They also feature automated machine data logging and aggressive in-house quality control, from hydrostatic pressure checks to high-speed tensile impact testing.
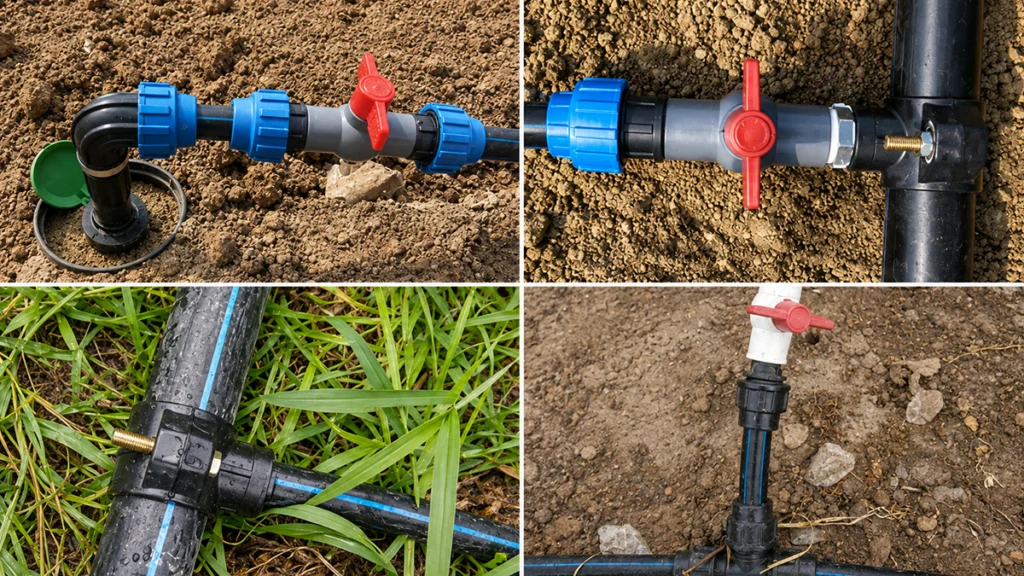
Here is the definitive breakdown of the top HDPE butt fusion fittings manufacturers for 2026. We judged them on production capacity, engineering precision, and their ability to deliver globally.
1. JINQUAN (China)
2. JM Eagle (USA)
3. Georg Fischer / GF Piping Systems (Switzerland)
4. Aliaxis (Belgium)
5. Wavin / Orbia (Netherlands)
6. ISCO Industries (USA)
7. AGRU (Austria)
8. Polypipe (UK)
9. Plasson (Israel)
10. Sunplast (China)
| Manufacturer | Country | Core Strength | Max Diameter | Key Certifications | Target Market |
|---|---|---|---|---|---|
| JINQUAN | China | 100K+ ton capacity, OEM | DN3000 | ISO 4427, CE, SGS | Global / Wholesale |
| JM Eagle | USA | 50-year warranty | 65" | NSF 61, AWWA | North America |
| Georg Fischer | Switzerland | RFID integration | DN1200 | EN 12201 | Europe / Industrial |
| Aliaxis | Belgium | Fluid management systems | DN1000 | WRAS, ISO 4427 | Global Infrastructure |
| Wavin | Netherlands | Sustainable piping | DN1200 | EN 12201, KIWA | Europe Municipal |
| ISCO Ind. | USA | Custom fabrication | 65" | ASTM F714 | Mining / Landfill |
| AGRU | Austria | Chemical transport | DN3000 | EN 12201 | Heavy Industrial |
| Polypipe | UK | UK market dominance | DN1000 | WRAS, BSI | UK Water Supply |
| Plasson | Israel | Precision molding | DN800 | WRAS, ISO 9001 | Gas & Water |
| Sunplast | China | Stock availability | DN800 | ISO 4427, CE | Export Wholesale |
Grasping the technical scope of a product range is non-negotiable for pipeline engineers. While standard injection-molded fittings usually span DN20 to DN1200, custom fabricated pieces can scale up to a massive DN3000 to support heavy infrastructure.
A high-caliber HDPE butt fusion elbow tee reducer factory provides a dense matrix of Standard Dimension Ratios (SDR) and pressure ratings:
| Fitting Type | Common Configurations | Size Range | Primary Function |
|---|---|---|---|
| Elbows | 90°, 60°, 45°, 22.5° (IPS/Metric) | DN20 – DN3000 | Changes pipeline direction smoothly to minimize flow turbulence. |
| Tees | Equal, Reducing, Y-Tees, Mud Tees | DN20 – DN2000 | Branches the pipeline; reducing tees handle diameter transitions. |
| Reducers | Concentric, Eccentric | DN25 – DN1200 | Transitions pipe sizes (e.g., 315mm x 250mm) while maintaining flow. |
| Stub Ends | Long spigot flange adapters | DN50 – DN1200 | Used with backing rings to bolt HDPE pipes to steel valves or pumps. |
| End Caps | Flat or domed | DN20 – DN1200 | Terminates the pipeline; requires stub end compatibility for testing. |
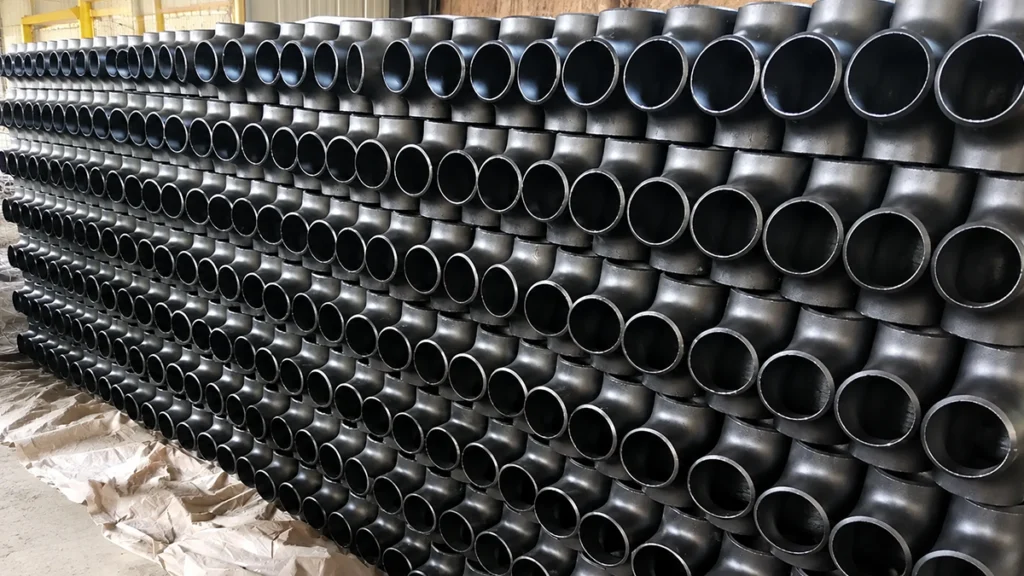
Every industrial application demands a distinct blend of material grades, pressure capabilities, and certifications. Matching your specific project requirements to the right manufacturer guarantees operational safety for decades.
City water infrastructure leaves no room for error, requiring absolute adherence to ISO 4427 / EN 12201 and stringent health approvals like NSF 61 or WRAS.
Gas networks face intense regulatory scrutiny and strictly mandate ISO 4437 compliance.
Mining environments brutalize piping systems with relentless abrasion and harsh chemical exposure.
Farming projects care about three things: cost-efficiency, UV resistance, and massive volume availability.
B2B wholesale buyers sourcing HDPE butt fusion fittings for distribution face a constant balancing act between unit cost and dependable delivery schedules. While resin market fluctuations influence exact pricing, the breakdown below offers realistic wholesale expectations for 2026.
| Parameter | Small Diameters (25mm – 63mm) | Medium Diameters (e.g., 90mm SDR11) | Large Diameters (e.g., 315mm+) |
|---|---|---|---|
| Indicative Price | $0.40 – $5.00 per piece | ~$2.10 per piece | $12.50 – $35.00+ per piece |
| Typical MOQ | 50 – 100 pieces per size | 10 – 50 pieces per size | 1 – 5 pieces per size |
| Standard Lead Time | 7 – 15 days (Stocked) | 7 – 15 days (Stocked) | 20 – 45 days (Fabricated) |
| Wholesale Basis | Quoted by 20ft/40ft container | Quoted by 20ft/40ft container | Quoted by 20ft/40ft container |
*Note: High-volume manufacturers like JINQUAN keep standard sizes heavily stocked, allowing them to hit rapid 7-15 day delivery windows. Conversely, custom fabricated orders almost always require a 20-45 day window to accommodate specialized production and rigorous QA testing.*
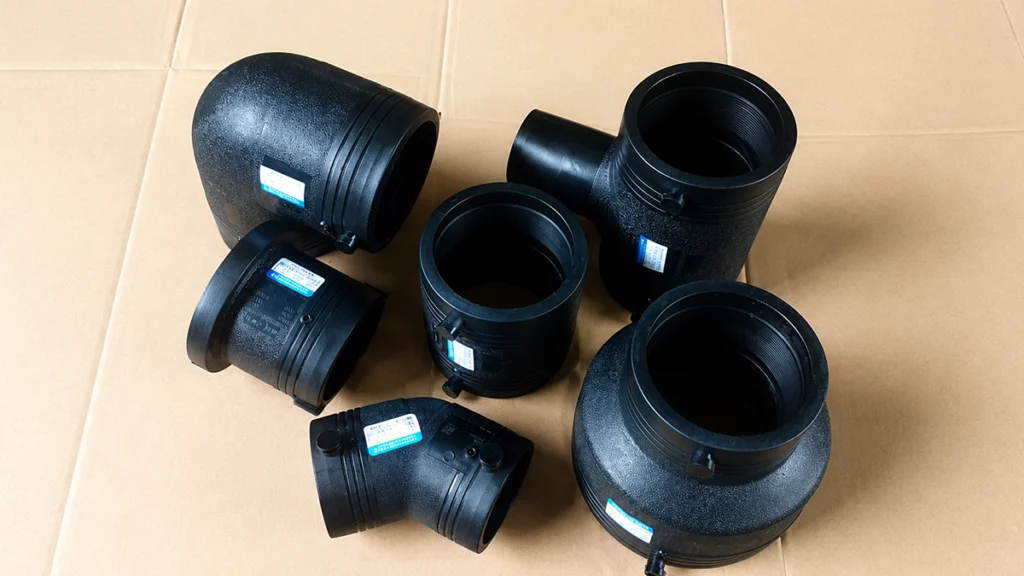
Buying from an unvetted custom OEM HDPE butt fusion fittings manufacturer—whether in China or elsewhere—invites severe risk. Protect your pipeline infrastructure by executing this step-by-step Quality Control (QC) verification workflow:
1. Material Certificate Verification: Always demand hard proof of 100% virgin PE100 resin. Scrutinize the Melt Flow Rate (MFR) and density metrics to guarantee zero regrind plastics made it into the batch.
2. Third-Party Lab Tests: Ask for recent hydrostatic pressure test reports and high-speed tensile impact results from recognized, accredited labs like SGS or TUV.
3. Factory Audit: Confirm ISO 9001 compliance firsthand. During your audit, check for automated data-logging systems on their injection molding machines. This technology guarantees consistent heating and cooling cycles.
4. Pre-Shipment Inspection: Measure dimensional tolerances yourself. Pay special attention to the outer diameter (OD) and wall thickness, comparing them strictly against ISO 4427-3 parameters.
Visual Red Flags on Fittings:
Do not hesitate to reject batches showing undersized fusion beads, asymmetrical flange curling, or heavy high-low misalignment at the joints. Surface pitting is another warning sign. Most dangerously, watch out for “cold welds.” These look perfectly fine to the naked eye but lack actual molecular bonding—a fatal flaw only exposed through destructive bend testing.
Even veteran procurement managers occasionally stumble when vetting a large diameter HDPE pipe butt fusion fittings supplier. Keep your project on track by avoiding these frequent pitfalls:
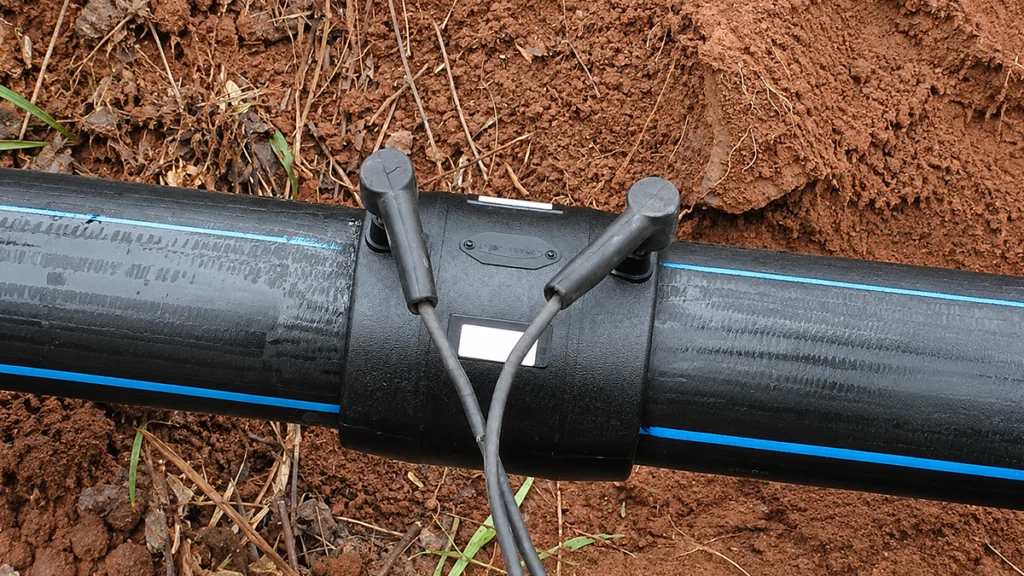
Mastering how to choose HDPE butt fusion fittings manufacturer partners ultimately decides the safety and financial success of your pipeline build. Run through this final procurement checklist before signing any supplier contracts:
Best Manufacturer by Use Case:
The heavyweights in this space include JM Eagle (USA), Georg Fischer (Switzerland), Aliaxis (Belgium), and JINQUAN (China). While JM Eagle and Georg Fischer control the heavily regulated Western markets, JINQUAN dominates high-volume, factory-direct manufacturing. With over 100,000 tons of annual capacity, JINQUAN supplies massive infrastructure, municipal, and agricultural projects across more than 50 countries.
Any trustworthy factory needs ISO 9001 for quality management and ISO 4427-3 (or EN 12201-3) to prove dimensional and structural integrity. If you are moving potable water, they must also carry health clearances like WRAS (UK) or NSF/ANSI 61 (North America). On the logistics side, CE and SGS certifications confirm they meet international export and third-party testing standards.
Costs swing wildly based on diameter and SDR ratings. Small components (25mm – 63mm) run anywhere from $0.40 to $5.00 a piece. Mid-sized items, such as a 90mm SDR11 elbow, hover around $2.10. Once you step into large diameters (315mm and up), expect to pay between $12.50 and $35.00+ per unit. Highly complex, custom fabricated large-diameter pieces will naturally push those prices much higher.
Absolutely, as long as they carry verified international credentials like ISO 4427, CE, and SGS. Elite Chinese factories, such as JINQUAN, rely entirely on 100% virgin PE100 materials, enforce automated quality control, and operate at massive scale. This gives buyers a distinct edge through factory-direct pricing and fast logistics for major global builds.
Minimum Order Quantities (MOQ) shift depending on the size of the fitting. Expect 50-100 pieces for small diameters, dropping to just 1-5 pieces for massive or custom parts. Wholesale deals usually price out by 20ft or 40ft containers. If you are buying standard stocked items, lead times sit between 7 and 15 days. Custom fabrications or enormous bulk orders stretch that window to 20 to 45 days.
Start by demanding a material certificate to confirm the use of 100% virgin PE100 resin. Next, ask for third-party hydrostatic pressure and tensile impact test reports. Run a factory audit to check for automated data-logging on their injection machines. Lastly, execute a pre-shipment inspection to measure the outer diameter (OD) and wall thickness against strict ISO 4427-3 limits.
Butt fusion suppliers create fittings that require a hot plate to melt the pipe ends before hydraulic pressure forces them together. Electrofusion suppliers, however, embed metal heating coils inside the fittings; applying an electric current melts the plastic from the inside out. Generally, butt fusion wins on cost for long, large-scale pipelines, while electrofusion is the go-to solution for tight trench repairs.
JINQUAN and AGRU stand out for large diameter water networks. JINQUAN leverages its massive scale to produce fittings up to DN3000, making them the most cost-effective choice for high-volume global projects. AGRU, meanwhile, earns high praise for supplying extreme industrial setups. Your final choice will depend entirely on your budget, regional certification needs, and project timeline.
Choosing the right HDPE butt fusion fittings manufacturer is an important step in ensuring reliable pipeline performance and controlling long-term project costs. Buyers should evaluate suppliers based on material quality, dimensional consistency, production capability, technical standards, and quality-control procedures.
For water supply, gas distribution, mining, and industrial pipeline projects, key factors include PE100 material compliance, applicable standards such as ISO 4427, SDR compatibility, molding quality, and third-party testing where required. Factory capability, production traceability, and technical support should also be considered before placing an order.
A careful supplier evaluation can help reduce compatibility issues, improve installation reliability, and support consistent performance throughout the service life of the pipeline system.